
10 Types of Screen Printing Inks for Vibrant Colors

Screen printing offers you several vibrant ink options including versatile pigment inks for exceptional color, eco-friendly neo-pigment Kornit inks for direct bonding, and water-based inks for soft breathable prints. You’ll find Superwhite and White Image Armor inks perfect for dark fabrics, while rubber inks excel in stretchable designs. Plastisol remains a popular choice for its durability and vibrancy. Understanding these ink types will help you create stunning custom prints that last.
Key Takeaways
- Plastisol ink delivers superior color vibrancy and versatility, making it the most popular choice for screen printing on both light and dark fabrics.
- Pigment ink provides exceptional color brightness and durability across various fabric types, especially cotton and polyester blends.
- Neo-Pigment Kornit ink offers vibrant colors through eco-friendly direct bonding in a single-step process.
- Metallic ink creates striking shimmer effects and premium appearance, requiring higher mesh count screens for optimal results.
- Glow-in-the-Dark ink produces luminescent effects on light fabrics, requiring multiple passes for maximum brightness.
Types of Screen Printing Inks for the Best Colors
You’ll find an exciting range of screen printing inks to achieve vibrant, long-lasting colors on your textile projects, from basic pigment inks to specialized metallic formulations. For the best results, you can choose between water-based options that work great on natural fibers, Neo-Pigment Kornit inks for digital precision, or high-opacity Superwhite ink that creates perfect coverage on dark fabrics. Whether you’re printing custom t-shirts or promotional items, each ink type offers unique properties and benefits that’ll help you nail the exact look you’re after.
1. Pigment Ink

Pigment ink stands as the most versatile and popular choice for screen printing applications. You’ll find these screen printing inks deliver exceptional color vibrancy and ink durability across various fabric types.
You can count on pigment ink to maintain its quality through repeated washing. It’s particularly effective on cotton and polyester blends.
When you’re working with light-colored fabrics, pigment ink offers excellent opacity. You’ll achieve crisp, clear prints that won’t fade easily.
The ink settles into the fabric’s fibers rather than just coating the surface. This means your designs will stay vibrant and professional-looking for years to come.
2. Neo-Pigment Kornit Ink

Neo-Pigment Kornit ink transforms digital textile printing with its eco-friendly water-based formulation. You’ll find its ink composition rivals traditional sublimation inks while offering superior sustainability.
Here’s what makes this innovative ink stand out:
- Zero harmful chemicals and low energy consumption
- Direct bonding with natural and synthetic fibers
- Single-step process without pre-treatment
- Vibrant colors that maintain wash fastness
You’ll appreciate how this next-gen ink eliminates the need for separate fixing agents. It’s transforming the industry with its one-step application process and minimal environmental impact. Whether you’re printing on cotton, polyester, or blends, Neo-Pigment Kornit delivers consistent, professional results.
3. Water-Based Ink

While traditional screen printing methods can be complex, water-based inks offer a simpler and more eco-conscious approach to textile printing.
You’ll find water-based inks are perfect for achieving soft, breathable prints on light-colored fabrics. They soak directly into the material instead of sitting on top.
These inks contain no harmful chemicals and create zero toxic waste. You’re making an environmentally responsible choice with eco-friendly printing.
The colors remain vibrant even after multiple washes. You’ll get excellent results on cotton, linen, and other natural fibers.
Keep in mind they work best on lighter fabrics. The drying time is longer than plastisol inks.
4. Superwhite Ink

Superwhite ink stands out as the powerhouse choice for achieving brilliant white prints on dark fabrics. You’ll find it’s specially formulated for maximum color vibrancy in screen printing.
When you’re working with dark garments, superwhite ink delivers these game-changing benefits:
- Superior opacity for crisp, clean prints
- Improved durability against washing and wear
- Excellent coverage without multiple passes
- Smooth finish with minimal fibrillation
You’ll notice the difference in your prints immediately. The ink’s high pigment concentration guarantees your designs pop with unmatched intensity. It’s particularly effective when you need that perfect white base layer for other colors.
5. Metallic Ink

Metallic inks add a striking shimmer and luxury feel to your screen printing designs. These specialty inks contain fine metallic particles that create an eye-catching reflective finish on your garments.
You’ll find metallic inks in popular colors like gold, silver, and copper. They’re perfect for creating premium-looking logos and designs that stand out from standard prints.
For best results with garment printing, you’ll want to use a higher mesh count screen. This helps prevent the metallic particles from clogging while ensuring smooth ink deposit.
Remember to cure metallic inks at the proper temperature. They typically need slightly longer drying times than standard inks.
6. Transparent Ink
Transparent inks create subtle yet impactful effects in screen printing by allowing the fabric’s color to show through. You’ll find these screen printing inks particularly useful for creating layered designs.
When you’re working with transparent ink in printing technology, you can achieve these stunning effects:
- Watercolor-like gradients that blend seamlessly
- Ghost images that appear three-dimensional
- Overlay effects that create new color combinations
- Depth and texture in your designs
You’ll want to test the transparency level on your specific fabric first. Different materials interact distinctly with transparent inks, affecting your final result.
7. Glow-in-the-Dark Ink
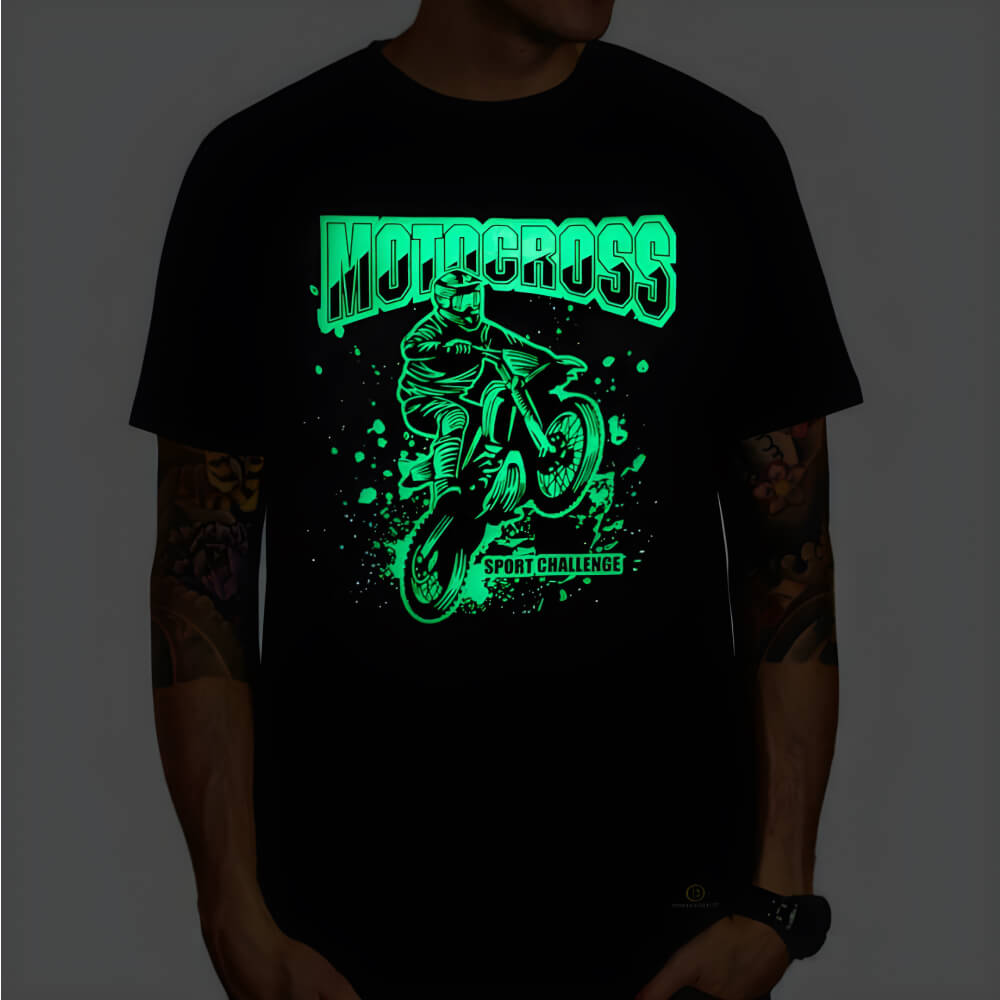
Glow-in-the-dark screen printing inks bring a magical luminescent effect to your designs. These specialty inks absorb light and release it slowly in dark conditions, creating an enchanting glow that’ll make your custom t-shirts stand out.
You’ll find these inks work best when printed on light-colored fabrics. They’re perfect for nightclub merchandise, concert shirts, and safety wear.
For maximum impact, expose your glow-in-the-dark ink designs to bright light before viewing in darkness. The glow typically lasts several hours.
Let’s investigate proper application techniques. You’ll want to use a higher mesh count screen and multiple passes to achieve the brightest results.
8. White Image Armor Ink

White Image Armor ink stands as a cornerstone in screen printing, delivering exceptional opacity and coverage on dark garments. You’ll find it’s perfect for t shirt printing projects that demand crisp, vibrant results.
When you’re working with this innovative ink, you’ll experience:
- Superior ink adhesion on various fabric types
- Flash-cure compatibility for multi-layer designs
- Smooth flow characteristics during application
- Extended shelf life with proper storage
This specialized ink guarantees your dark garment prints maintain their brightness and durability through multiple washes. You’ll appreciate how it prevents fibrillation while providing excellent coverage on challenging substrates.
9. Rubber Ink

Building on our ink exploration, rubber-based screen printing inks bring exceptional flexibility and stretchability to your textile projects.
You’ll find these inks offer similar qualities to plastisol inks but with improved elasticity for stretchy fabrics. They’re perfect when you need your designs to move with the material.
For high density printing, rubber inks create raised effects that maintain their shape even after repeated stretching. You’ll get impressive durability and wash-fastness too.
These inks work best on athletic wear, swimsuits, and performance garments. You’ll appreciate how they resist cracking while providing that soft, flexible feel your customers love.
10. Plastisol Ink

Screen printers overwhelmingly choose plastisol inks as their go-to option for vibrant, long-lasting results. These industrial printing inks dominate the textile printing market for good reason.
You’ll find plastisol inks excel in several key areas:
- Superior color vibrancy that won’t fade over time
- Excellent opacity on both light and dark fabrics
- Long shelf life without drying or curing until heat-activated
- Versatile application across various fabric types
You don’t need to worry about these inks drying in your screen. They’ll stay workable until you’re ready to cure them with heat. It’s the perfect choice when you need reliability and consistency.
Conclusion
While choosing screen printing inks may seem overwhelming at first, partnering with established suppliers like Texco can make your selection process much simpler. You’ll find expert guidance to achieve ideal print quality and color accuracy for your specific needs.
Remember that each ink type serves different purposes and materials. You’re now equipped to make informed decisions based on your project requirements.
Consider factors like fabric type, durability needs, and production scale when selecting your inks. With proper research and supplier support, you’ll create stunning prints that meet both your creative vision and practical demands.
The custom apparel market is projected to reach $8.2 billion by 2028, showing the growing demand for quality printing solutions.
Let Texco’s expertise guide your printing journey to success.